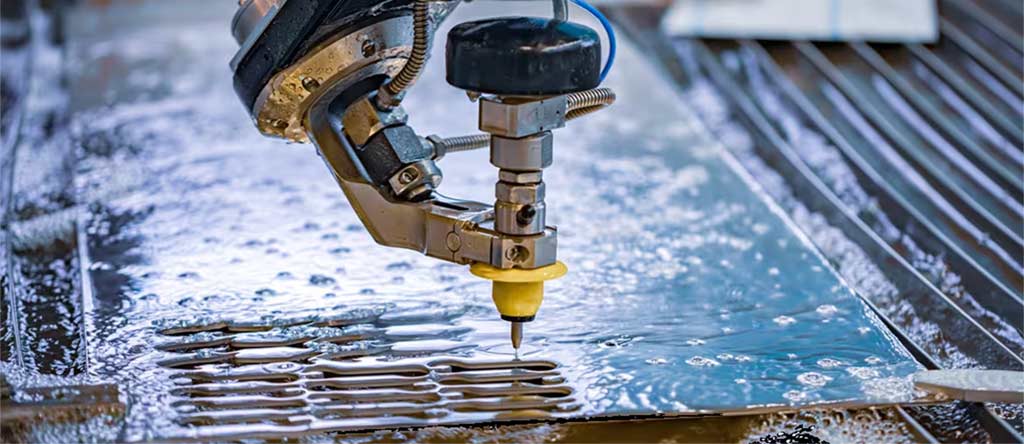
Water jet cutting. High-pressure water blasting through material. Sometimes mixed with abrasive grit. Cuts everything from soft plastics to hardened metals. Crazy precise. And here’s the kicker—no heat damage. None. That matters more than most people realize.
Snapshot: What You Should Know
| Feature | Details |
| How Tight | ±0.1 mm or better. Pretty darn accurate. |
| What It Cuts | Foam, rubber, plastics, metals, glass, stone, and composites. The list goes on. |
| Heat Generated | Zero. No heat-affected zone. Cold- cutting all the way. |
| Typical Cost (USA) | $80–$150 per hour. Depends on material and thickness. |
| Best For | Intricate shapes, heat-sensitive materials, prototypes, and short-run parts. The finicky stuff. |
How Water Jet Cutting Actually Works
Pretty simple concept. Water gets pressurized. Like, insanely pressurized. We’re talking 50,000 PSI or more. That stream blasts through a tiny precision nozzle, and CNC automation guides it along whatever path you need.
Two main flavors here:
Pure Water Jet Cutting
Just water. No additives. Perfect for soft or flexible stuff—foam, rubber, textiles, plastics, paper, and even some food products. Because there’s no abrasive mixed in, the material stays clean. Big deal for medical, food-grade, or contamination-sensitive parts.
Abrasive Water Jet Cutting
Harder materials need more punch. So you add abrasives—usually garnet—to the water stream. That turns the jet into a serious erosion tool. Steel, aluminum, titanium, glass, ceramics, stone, carbon fiber, and composite laminates. All fair game.
And still no heat. That’s the whole advantage over laser and plasma. Material properties stay intact.
Benefits of Water Jet Cutting
No Heat-Affected Zone
Cold process. Material doesn’t warp, discolor, or harden. Huge deal for aerospace alloys, composites, plastics, tool steels, and thin-wall parts. Original mechanical and chemical properties? Still there. Untouched.
High Precision and Smooth Edges
Water jet machines hit tight tolerances routinely. Edges come out smooth—often need zero secondary finishing. Perfect for intricate patterns, tight corners, and detailed features.
Cuts Almost Anything
Soft foam to hardened steel. Doesn’t matter. Water jets handle an absurdly wide range of materials. No tool changes. No special setups. Just cut.
Environmentally Friendly
No smoke. No toxic fumes. Minimal dust. Minimal waste. The garnet abrasive? Recyclable in many facilities. Greener than you’d expect.
Efficient Material Usage
Super thin kerf. That’s the cut width. Means tighter nesting on your sheets, less scrap in the bin. Lower cost. More sustainable production. Win-win.
Where Water Jet Cutting Gets Used
Precision plus flexibility plus clean operation. That combo works across a ton of industries.
Aerospace and Automotive
Brackets. Interior panels. Composite structures. Engine components. Water jets protect expensive materials from distortion and keep structural integrity intact.
Medical and Healthcare
Precision and cleanliness make it perfect for implant components, surgical tools, and prototyping medical devices. Contamination isn’t an option in that world.
Architectural and Construction
Intricate flooring patterns. Decorative metals. Tile and stone inlays. Countertops. Signage. The aesthetic stuff where precision actually shows.
Electronics
No heat means no damage to sensitive components. Circuit board panels. Device enclosures. Thin metals and plastics. Works great.
Industrial Equipment
Gaskets. Seals. Brackets. Machine components. The everyday industrial stuff that keeps everything running.
Water Jet Cutting vs. Other Methods
Water Jet vs. Laser
A water jet gives you no heat, cuts thick materials, and handles reflective metals. Laser is faster with very clean edges but creates heat-affected zones. Pick based on what you’re cutting.
Water Jet vs. Plasma
Water jet offers high precision, no heat, and works on thinner or sensitive materials. Plasma is faster on thick metals but leaves rougher edges and heat distortion. Tradeoffs.
Water Jet vs. CNC Machining
Water jet is faster for flat profiles, lower cost for certain shapes, and less setup time. CNC machining wins when you need precise holes, threads, or 3D geometry. Different tools for different jobs.
Water jets get picked a lot for flat-profile parts or materials that can’t handle heat. Makes sense.
What Affects Water Jet Cutting Cost?
Pricing varies. But here’s what drives the numbers:
Material Type. Harder or thicker materials take more time and are more abrasive. Simple physics.
Material Thickness. Thicker parts slow down the cut speed. More machine time. Higher bill.
Edge Quality Required. Want cleaner edges? Slower cutting speeds. That’s the tradeoff.
Geometry Complexity. More turns, internal features, and tight tolerances—all add time.
Quantity. Water jets are great for prototypes and short runs. But cost per part drops with higher volume. Always does.
Step-by-Step Water Jet Cutting Process
Here’s how a project goes from idea to finished part:
Step 1: CAD File Creation. A 2D profile gets created or refined. Styner Machine Tools can help with CAD engineering if needed.
Step 2: Material Selection. The right material gets sourced and prepped for cutting.
Step 3: CNC Programming. The toolpath is generated based on the thickness and edge quality requirements.
Step 4: Water Jet Cutting. Machine-cuts along the programmed path. Extreme accuracy.
Step 5: Quality Check. Tolerances, edge conditions, and dimensions are all verified.
Step 6: Final Finishing (If Needed). Some parts need deburring, cleaning, or secondary machining. Many water-jet parts need none. Done.
Current Trends in Water Jet Cutting (USA)
Higher-pressure systems are cutting times down. Faster jobs. Better margins.
Improved abrasive recycling is reducing cost and waste. Shops are getting smarter about it.
Hybrid machining workflows combining water jets with CNC finishing are becoming standard. Best of both worlds.
Demand keeps growing in aerospace, custom fabrication, robotics, and EV manufacturing. The water jet isn’t going anywhere.
FAQs
What materials cannot be cut with a water jet?
Tempered glass is the main one—it’ll shatter. Most other materials? Fair game.
How thick can a water jet cut?
Industrial systems handle metal over 6 inches thick. Depends on the material and what edge quality you need.
Does water jet cutting leave burrs?
Very few. Edges usually come out smooth with little to no finishing required. One of the perks.
Is water jet cutting good for prototypes?
Absolutely. Fast setup, precise shapes, no tooling. Ideal for one-off parts or small batches.
Is water jet cutting accurate?
Many machines hit ±0.1 mm or better. Plenty accurate for detailed industrial parts.
How does a water jet compare to a laser for metals?
Laser is faster on thin metals. Waterjet wins on thick materials and anything heat-sensitive. Pick based on the job.
Why Styner Machine Tools
Styner Machine Tools provides advanced water jet cutting, CNC machining, and metal fabrication services for shops and manufacturers across the USA.
Prototypes. Short-run production. Complex components. Our team delivers accuracy, fast turnaround, and solid engineering support.
Need precision cutting without the heat? Styner Machine Tools. Let’s get it done.